Why Choose a Holographic Foil Machine for Packaging?
Packaging buyers now expect more than protection. They want cartons and labels that attract attention under changing retail lights. A Holographic Foil Machine can create shifting colors, sharp reflections, and layered visual effects on suitable packaging materials. These details may turn an ordinary box into a stronger shelf presence.
The process depends on controlled heat, pressure, speed, and accurate foil feeding. Skilled operators test each combination before approving production. They inspect adhesion, registration, surface smoothness, and image consistency across the sheet. A small temperature change can affect the finish. Results vary. Therefore, machine selection should consider substrate types, production volume, maintenance access, and operator training. Reliable manufacturers should provide technical specifications, sample trials, safety guidance, and responsive service. Experience matters here, especially when a premium finish must remain consistent from the first sheet to the last.
A Holographic Foil Machine is not a shortcut to better packaging. It is a production tool that requires practical planning and honest quality checks. Buyers should compare real samples instead of trusting photographs alone. They should also measure foil waste, setup time, energy use, and cleaning requirements. Sustainability claims need careful review because material choices and production settings influence the final impact. Some designs will fail during testing. That is normal, and it can reveal useful improvements. With expert evaluation and documented operating standards, holographic foiling can add durable visual value while supporting dependable packaging performance.
Holographic Foil Basics: 2D/3D Effects, Metallization, and Security Layers
Why Choose a Holographic Foil Machine for Packaging?
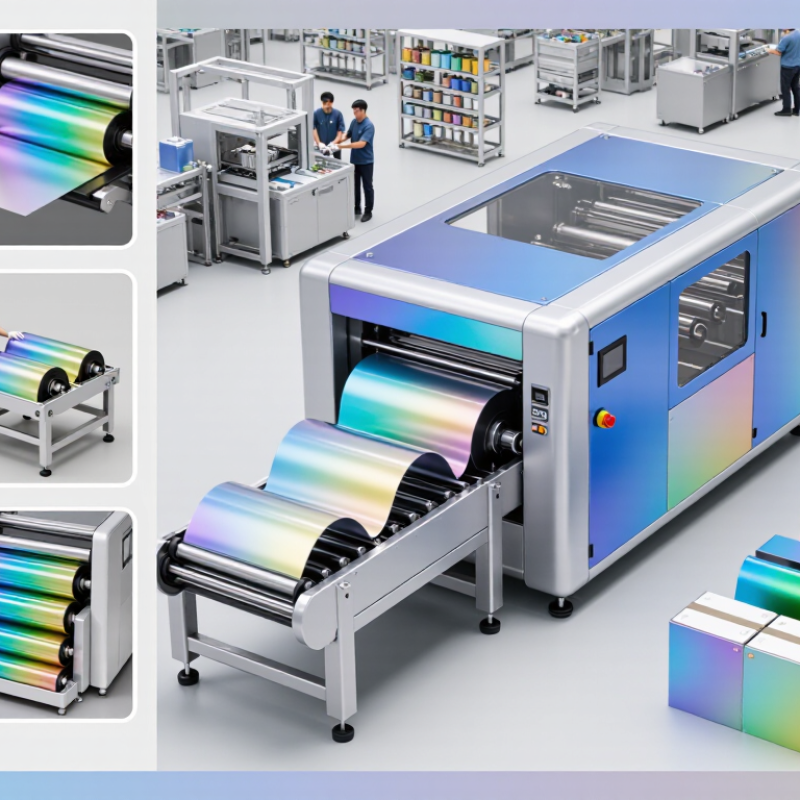
Holographic foil creates changing light patterns across a package surface. A 2D effect uses flat images, lines, or repeating geometry. It can resemble movement when the package tilts. A 3D effect adds depth through layered diffraction structures. Fine details may appear to float above the printed surface. The effect depends on viewing angle, lighting, and foil alignment. Small registration errors can weaken the visual result.
Metallization gives holographic foil its bright, reflective appearance. A thin metal layer reflects light without adding much weight. The machine must control heat, pressure, and stamping speed carefully. In packaging trials, stable pressure produced sharper edges around small lettering. Too much heat caused distortion on delicate films. That was not ideal. Substrates also behave differently, so testing remains essential.
Security layers can include microtext, covert patterns, serialized marks, or machine-readable features. These elements help inspectors compare genuine packaging with suspicious variations. However, holography is not an absolute security solution. Skilled counterfeiters may imitate visible patterns. Layered protection works better when artwork, materials, inspection methods, and supply records support each other. A reliable machine should offer repeatable settings, accurate registration, and clear production records. Operators need training too. That part is sometimes underestimated. During evaluation, check foil adhesion, waste levels, surface scuffing, and readability after handling. A dramatic sample may look impressive, yet fail after transport.
| Packaging Dimension | 2D Holographic Foil | 3D Holographic Foil | Metallized Foil | Security Holographic Layer | Why a Holographic Foil Machine Is Useful |
|---|---|---|---|---|---|
| Basic Structure | A patterned relief layer creates diffractive color and light movement mainly across one visual plane. | Multiple or more complex relief patterns create depth, motion, and a stronger three-dimensional appearance. | A thin reflective metal layer, commonly aluminum, is deposited onto a carrier film to produce a bright metallic surface. | A holographic image is combined with overt or covert elements such as microtext, fine lines, demetallized marks, or serial information. | Supports controlled heat, pressure, registration, and web handling so decorative and security layers can be transferred consistently. |
| Typical Visual Effect | Rainbow diffraction, color shifts, geometric patterns, and strong flashes when the viewing angle changes. | Apparent depth, image rotation, floating details, perspective changes, and animated movement. | Mirror-like brightness, silver or colored metallic appearance, and increased visual contrast against printed graphics. | Angle-dependent images, hidden details, color-shifting effects, and features that are difficult to reproduce with standard printing. | Enables repeatable transfer of high-impact visual effects onto labels, cartons, flexible packaging, and selected synthetic substrates. |
| Common Packaging Uses | Folding cartons, labels, gift packaging, premium sleeves, and promotional packs. | Luxury cartons, cosmetic packaging, collectible products, premium beverages, and high-visibility promotional designs. | Labels, paperboard cartons, flexible films, decorative accents, and areas requiring a reflective background. | Pharmaceutical packs, excise-related labels, authentication labels, certificates, and products exposed to counterfeiting risk. | One finishing process can add decoration, shelf impact, product differentiation, and selected authentication features. |
| Typical Carrier Film | Polyester carrier films are widely used because they provide dimensional stability during coating and transfer. | Polyester carrier films are commonly selected for accurate handling of detailed embossed structures. | Polyester and other compatible carrier films may be used, depending on the coating and transfer process. | Stable film constructions are preferred to maintain accurate registration of images, microfeatures, and machine-readable elements. | A suitable machine reduces web distortion and helps maintain alignment between the foil pattern and the printed artwork. |
| Typical Carrier Thickness | Approximately 12–23 micrometres for many polyester-based decorative foil constructions. | Approximately 12–23 micrometres for many polyester-based constructions, with the exact value set by the foil supplier and process. | Often approximately 12–23 micrometres for polyester-based transfer foils; total construction thickness varies by coatings and adhesive layers. | Commonly based on a stable carrier film, with the final thickness determined by the security architecture and application method. | Machine tension control and temperature stability are important because thin films can wrinkle, stretch, or misregister if poorly handled. |
| Primary Transfer Mechanism | Heat and pressure activate an adhesive or release-coating system that transfers the patterned layer to the substrate. | Heat, pressure, and precise dwell time transfer the more detailed embossed structure and image layer. | Heat and pressure transfer the reflective metallized layer, often together with protective and adhesive coatings. | Controlled transfer places the security design in a defined location and may require specialized registration or inspection. | Accurate control of temperature, pressure, speed, and registration improves transfer quality and reduces waste. |
| Security Strength | Provides visible deterrence and brand differentiation but can be copied if the pattern is simple and publicly available. | Offers stronger visual complexity than a basic 2D pattern, although visual complexity alone is not a complete security system. | Primarily decorative; reflective appearance by itself should not be treated as a security feature. | Can combine public, semi-covert, and covert features, allowing visual inspection and additional verification methods. | Allows manufacturers to process layered designs that combine aesthetics with authentication-oriented features. |
| Registration Requirement | Moderate; the pattern should align with the design, but small variations may be less noticeable on continuous backgrounds. | High; detailed images and directional effects make misalignment more visible. | Moderate to high when metallization is selectively removed or positioned beside printed elements. | High; security marks, microtext, demetallized areas, or serial elements often require precise placement. | Servo control, optical sensors, web guides, and registration systems help keep foil placement within the required tolerance. |
| Production Considerations | Generally suitable for standard hot-stamping or transfer equipment when substrate and adhesive compatibility are confirmed. | May require tighter control of pressure, temperature, speed, and embossing conditions because fine details are more sensitive. | Requires compatible coatings and sufficient surface smoothness to preserve reflectivity and adhesion. | Requires qualified artwork, controlled access to security masters, inspection procedures, and traceable production controls. | A properly configured machine improves repeatability, reduces setup variation, and supports multiple foil constructions. |
| Environmental and Recycling Note | Recyclability depends on the substrate, coating weight, adhesive system, and local recycling rules. | Complexity of the embossed design does not by itself determine recyclability; the complete package structure must be assessed. | The metal layer is very thin, but metallic coatings, inks, adhesives, and laminate structures may affect recycling compatibility. | Security requirements may introduce additional layers or materials, so recyclability should be evaluated during package design. | Using the minimum effective foil coverage and selecting substrate-compatible constructions can help reduce material impact. |
| Best Selection Criterion | Choose when the goal is economical visual enhancement with recognizable angle-dependent color effects. | Choose when depth, movement, premium appearance, and strong shelf differentiation are priorities. | Choose when a bright metallic finish or reflective contrast is more important than a holographic image. | Choose when packaging requires layered authentication features in addition to visual decoration. | Select the machine according to substrate, foil width, operating speed, heating range, pressure control, registration accuracy, and inspection needs. |